◇
Press brakes
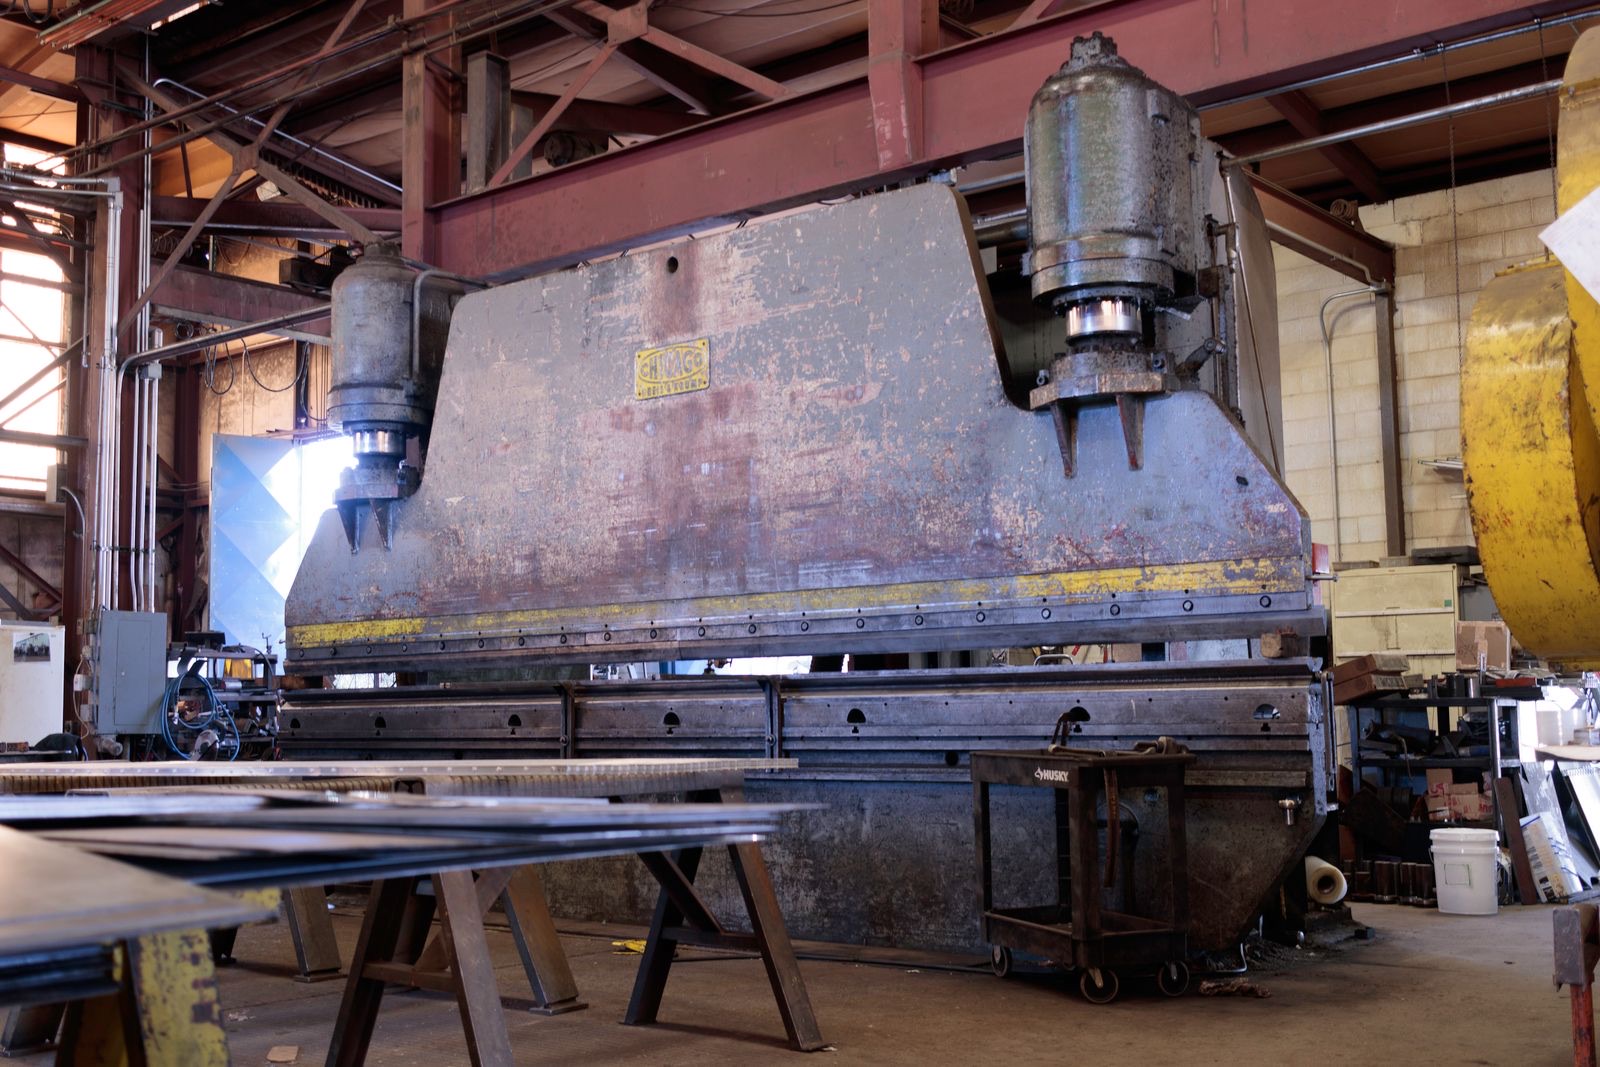
Main cylinders and crowning cylinders; synchronised pairs with position feedback.
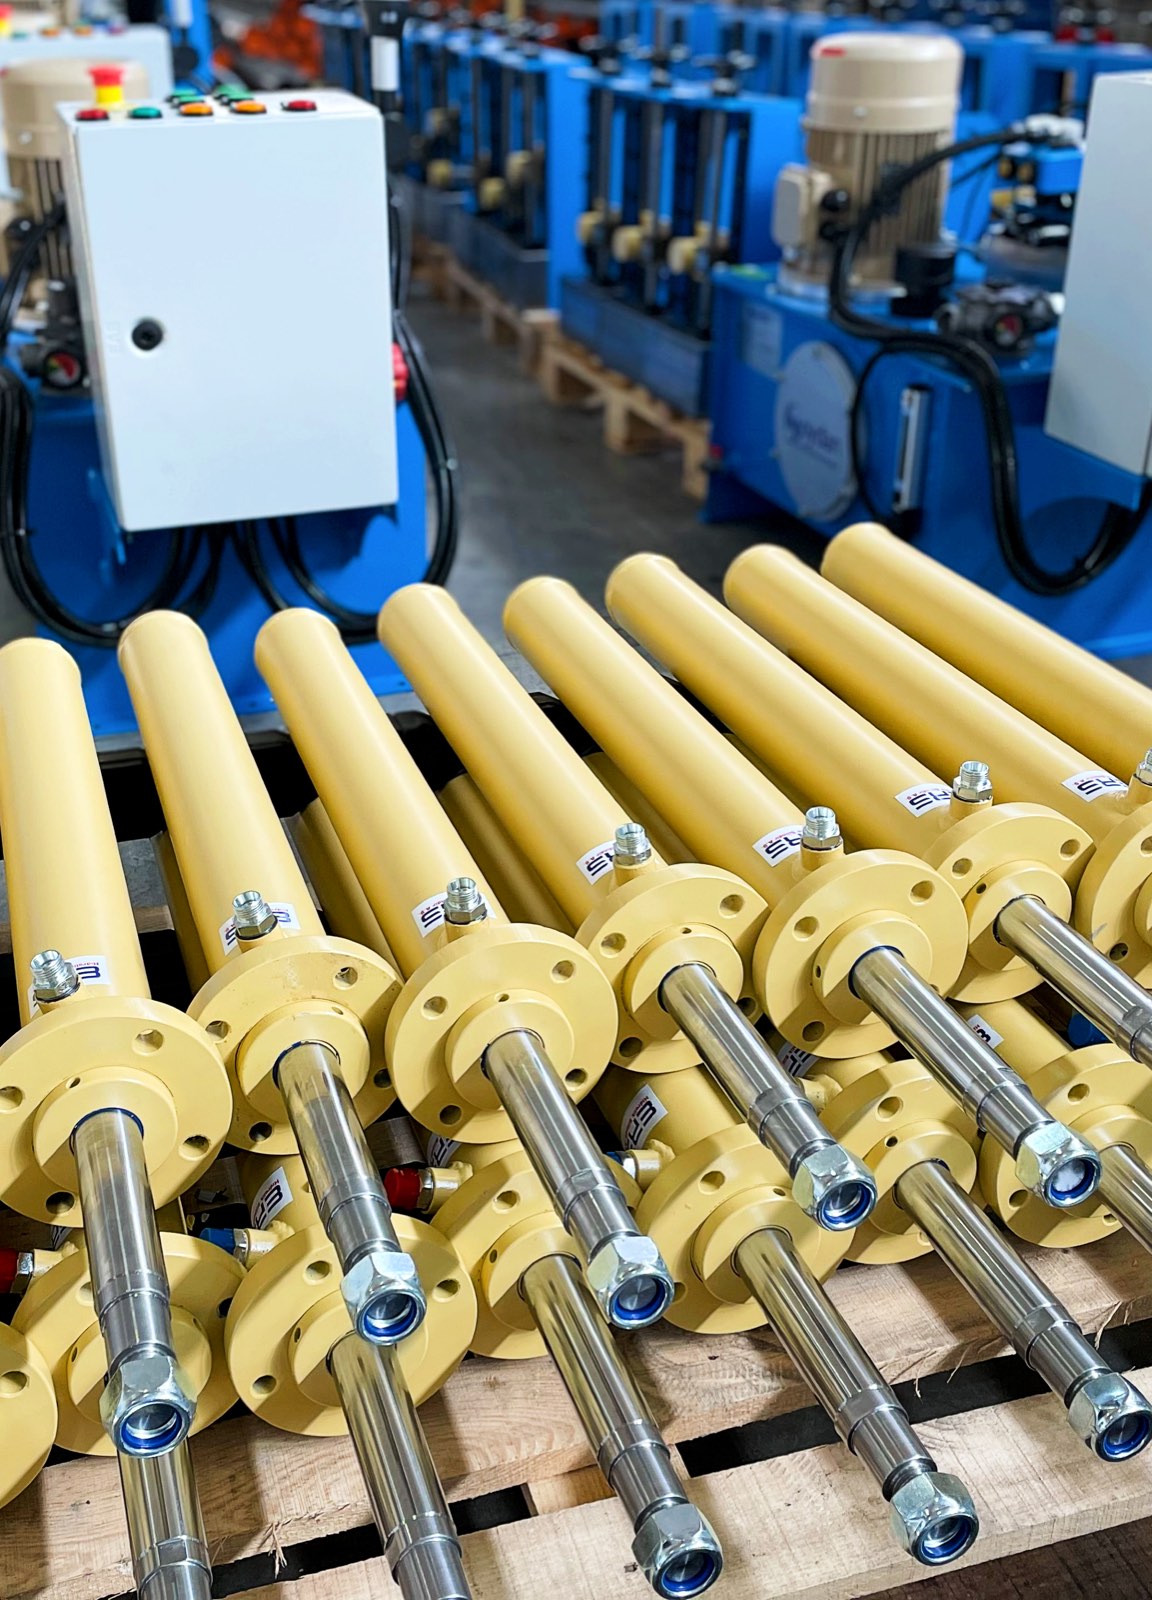
The main cylinder sets the tonnage and the accuracy of a press. Soydan Hidrolik manufactures ISO 6022 round-flange, welded heavy-duty and position-feedback servo cylinders in İzmir for press brakes, deep-drawing presses, plate rolls and balers. Every cylinder, synchronised pairs included, is tested to ISO 10100 at working pressure and at 1.5× working pressure, and ships with a serialised test report. We supply OEM cylinders in series to exporting metalworking machinery manufacturers, and ship to Germany, Austria and the United Kingdom.
Across the full Hydrocyl cylinder range, standard production covers bores Ø25–400 mm, rods Ø16–280 mm and strokes to 4,000 mm. Project cylinders go to Ø1,000 mm bore, Ø700 mm rod, 12 m stroke and 400 bar; see large-bore and custom hydraulic cylinders. Catalogue and certificates: downloads.
Values are the theoretical push force on the full-bore side, with friction neglected; with p in bar and D in mm, F [kN] = p × π × D² / 4 / 10,000. The table is for a quick first selection; final sizing takes account of speed, duty cycle, safety factor and buckling, and is verified by our engineers at quotation stage.
| Bore | 200 bar | 250 bar | 350 bar |
|---|---|---|---|
| Ø80 mm | 101 kN | 126 kN | 176 kN |
| Ø100 mm | 157 kN | 196 kN | 275 kN |
| Ø125 mm | 245 kN | 307 kN | 430 kN |
| Ø160 mm | 402 kN | 503 kN | 704 kN |
| Ø200 mm | 628 kN | 785 kN | 1,100 kN |
| Ø250 mm | 982 kN | 1,227 kN | 1,718 kN |
| Ø320 mm | 1,608 kN | 2,011 kN | 2,815 kN |
| Ø400 mm | 2,513 kN | 3,142 kN | 4,398 kN |
An illustrative example: a single Ø200 mm piston develops 80 tonnes (≈785 kN) of push force at 250 bar. In a synchronised twin-cylinder set, two Ø160 mm pistons give about the same force at 200 bar (2 × ≈402 kN ≈ 82 tonnes); at 250 bar the same set delivers ≈1,005 kN, just over 100 tonnes. A twin-cylinder layout also spreads the force along the ram. Sketch your own cylinder in the Drawing Studio and request a quote.
On press brakes and large die presses, how closely the two cylinders keep the same speed and position decides bending-angle accuracy and die life. We therefore build them as matched sets, not as individual units: the tubes are honed to ISO H8 tolerance and the stroke behaviour of both cylinders is compared on the same test bench.
For position-controlled presses the cylinders can be supplied with an integrated linear sensor, ready for closed-loop synchronisation with a proportional valve and controller. On request we design the valve manifold and hydraulic power unit alongside the cylinders.
We build press brake, punching and plate-rolling cylinders in series as an OEM supplier to exporting machine builders; Akyapak, the Bursa-based metalworking machinery manufacturer, is among our customers. Applications and family matching are on the Presses & Metalworking sector page; for supplier selection criteria, see choosing a hydraulic cylinder manufacturer.
Cylinders are built at our works in the İzmir Atatürk Organised Industrial Zone (Çiğli) and shipped in ISPM-15 heat-treated crates, with Incoterms agreed per order. European accounts are handled from our London office (UK supply, contact), and factory audits are welcome. The 12-month warranty is set out in our terms of sale; for what drives cylinder pricing, see hydraulic cylinder cost.
Press cylinders run for millions of cycles; design details that cannot be seen from outside decide their life. At quotation stage we review these six points against your application.
Cylinder, valve manifold, accumulator and power unit can be designed together as one press circuit; see hydraulic power units and engineering projects.
An illustrative scenario: 100 tonnes (≈981 kN) of bending force, 250 mm stroke, 250 bar working pressure, a synchronised ram on two cylinders. Each cylinder must deliver ≈490 kN; from the table, a Ø160 mm piston gives ≈503 kN at 250 bar. To allow for friction and a safety margin, Ø180 mm (≈636 kN) may be preferred to Ø160. With a short stroke and flange mounting, buckling does not govern; the side load on the ram during bending and the choice of guide rings do.
The tubes of both cylinders are honed to ISO H8 and their stroke behaviour is matched. On press brakes, position feedback usually comes from frame-mounted linear scales; on request the cylinders are supplied with an integrated linear sensor. Closed-loop control with proportional valves keeps the ram parallel throughout the stroke. Small-bore cylinders can be added to the lower beam for crowning. This example is for pre-sizing only; for a firm selection, send the press data on the quote form.
For standard tonnages, the ISO 6022 round-flange HYC-F family (Ø50–400 mm, 250 bar nominal / 350 bar maximum) is the usual choice. Where higher pressure or a design built to drawing is needed, the welded heavy-duty HYC-W is used (to 400 bar on a project basis); for a position-controlled ram, the servo HYC-S.
The tubes of both cylinders are honed to ISO H8 tolerance, and their stroke behaviour is compared and matched on the test bench. Sets with position feedback come with an integrated linear sensor, ready for closed-loop synchronisation.
Force is working pressure multiplied by piston area: F = p × A, with p in MPa (1 bar = 0.1 MPa) and A in mm² (A = π × D² / 4); the result is in newtons. With p in bar and D in mm, F [kN] = p × π × D² / 4 / 10,000. For example, a Ø200 mm piston at 250 bar produces about 785 kN (≈80 tonnes). The table values are for pre-sizing; our engineers make the final calculation with friction, speed and safety factor included.
Yes. Send the cylinder or its dimensions; we reverse-engineer it, produce the drawing and manufacture a like-for-like replacement; on request we propose improvements to sealing and materials. The delivery schedule is planned with you to keep press downtime short.
Custom press cylinders are ready ex-works in under 10 weeks after drawing approval; Incoterms are agreed per order and cylinders ship in ISPM-15 crates. Every cylinder is tested to ISO 10100 at working pressure and at 1.5× working pressure; a signed, serialised test report and the engineering file are delivered with it. Tubes and rods are European; seal sets come from Kastaş, Trelleborg and European brands. Soydan Hidrolik is certified to ISO 9001, ISO 14001 and ISO 45001.
Give us press type, force (tonnes or kN), stroke, working pressure, duty cycle, mounting style and quantity, with drawings as PDF, DWG or STEP if available; we reply within 48 hours with an application data sheet.
Instant Quote → WhatsApp