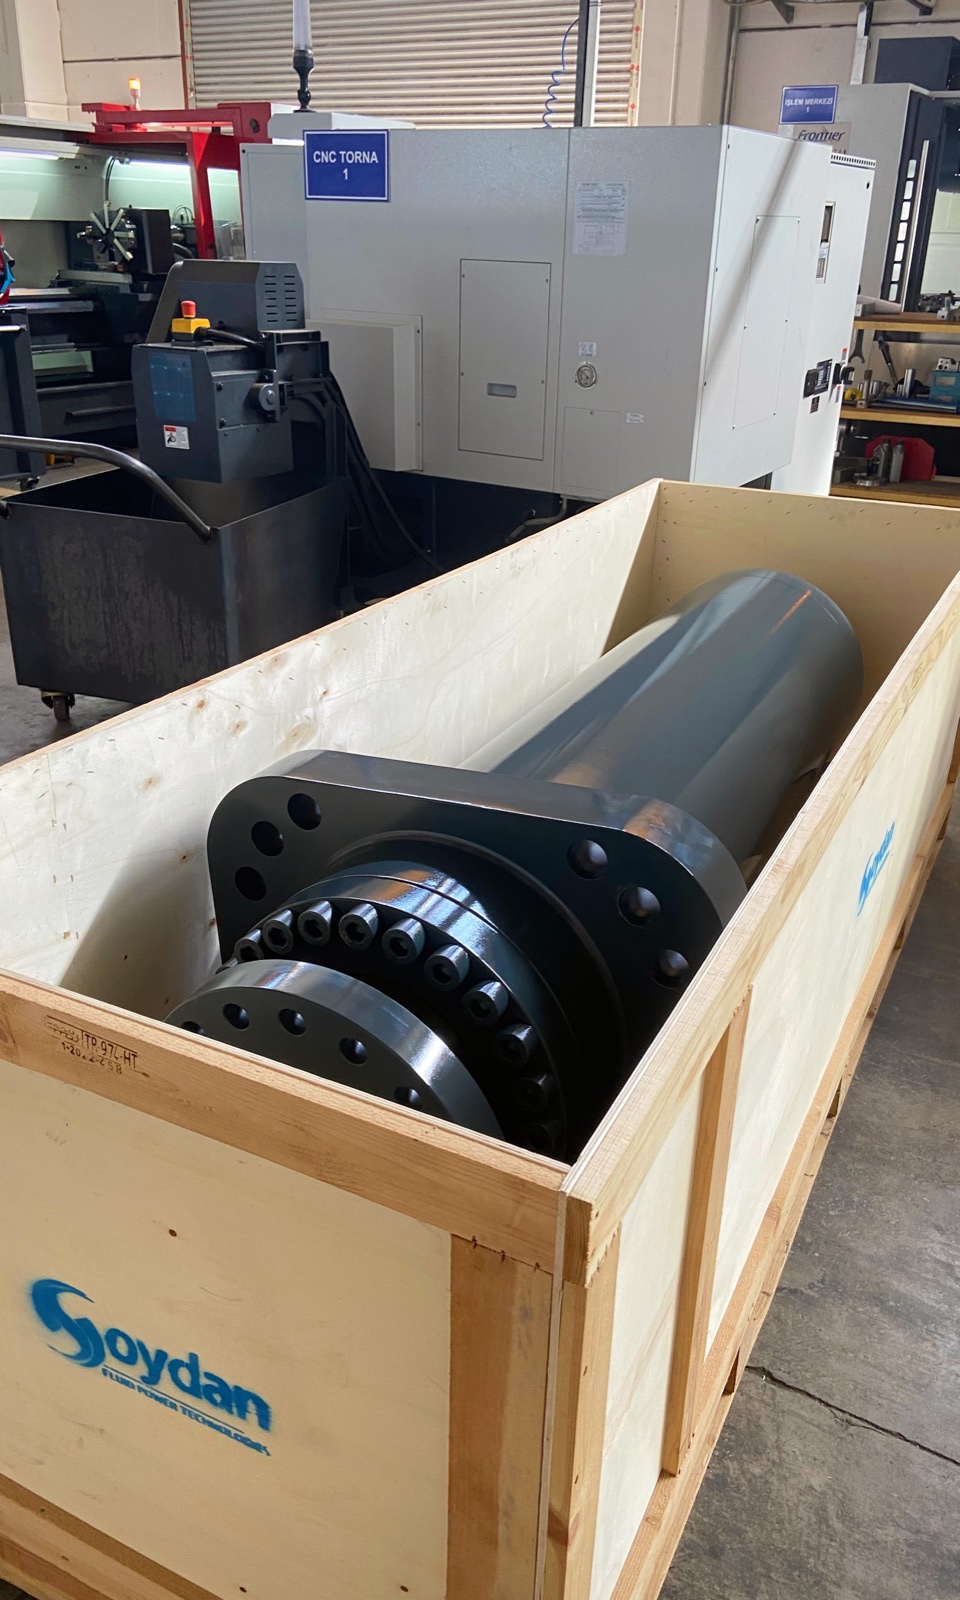
[Ø]Large bore · long stroke · project manufacture

Large bore hydraulic cylinders: to Ø1,000 mm bore, 12 m stroke, 400 bar.

Standard production at Soydan Hidrolik covers bores of Ø25–400 mm, rods of Ø16–280 mm and strokes to 4,000 mm. Beyond that, we design and build project cylinders at our İzmir works to Ø1,000 mm bore, Ø700 mm rod, 12 m stroke and 400 bar. Welding is carried out under EN ISO 3834-2 with NDT of welds; every cylinder is pressure tested to ISO 10100.

[01]Project capacity

Above the standard range.

Ø1,000 mm
Bore · project ceiling (standard: Ø400 mm)
Ø700 mm
Rod · project ceiling (standard: Ø280 mm)
12,000 mm
Stroke · project ceiling (standard: 4,000 mm)
400 bar
Working pressure · project ceiling

These are ceilings; each combination of bore, stroke and pressure is verified by calculation. Above the standard range every cylinder is a project: buckling and strength calculations, weld joint design and a test plan are completed before manufacture, and 2D/3D drawings go to you for approval. The welded HYC-W family is the basis; ISO 6022 round-flange (HYC-F) and mill-type (HYC-M) constructions are also built as projects. For the build-to-drawing process, see custom hydraulic cylinders.

[02]Six critical points, design to dispatch

What changes at large bore?

◇
Buckling
On a long stroke hydraulic cylinder, buckling rather than force usually sets the rod diameter. Mounting style and installed position give the buckling length; Euler or Tetmajer is applied, depending on rod slenderness, with a safety factor. If necessary the rod diameter is increased or a stop tube lengthens the bearing span.
◇
Welding and body
Thick-walled welded bodies depend on joint design, preheating, post-weld stress relief where required and non-destructive testing (NDT). Welding is carried out under EN ISO 3834-2; NDT Level II certified personnel inspect the welds.
◇
Rod weight and sealing
From Ø300 mm rod diameter upwards, rod mass and sag put side load on the gland bearing and rod seal. Heavy-duty seal sets and wide guide rings from Kastaş, Trelleborg and European brands are selected to suit.
◇
Honed tube and chromed rod
At large diameters and long lengths, surface roughness (Ra), straightness and roundness are critical; the honed tube and hard-chromed rod are ordered from European mills to the project dimensions.
◇
Testing
Every cylinder is tested to ISO 10100 at working pressure and at 1.5 times that. The oil volume and test rig are planned at project start; the test report is signed and serialised.
◇
Logistics
A 12 m stroke means a closed length of over 13 m, so the cylinder ships as a special load: ISPM-15 heat-treated timber crate, rod protection, marked lifting points. Packing and Incoterm are stated in the quotation.
[03]Applications

Where are large bore cylinders used?

◇
Steel plants
Large bore, heavy-duty mill cylinders for continuous casters, rolling mills and furnace charging machines, built for heat, scale and round-the-clock operation. Details →
◇
Marine and shipbuilding
Hatch cover, ramp and deck crane cylinders; nickel-chrome duplex or HVOF tungsten-carbide rod coating for marine duty, class documentation on request. Details →
◇
Mining and heavy plant
High loads, shock, dust and mud; heavy-duty welded body, reinforced bearing arrangement and project-specific rod coating. Details →
◇
Large presses
High-tonnage main press cylinders; 350–400 bar working pressure, integrated cushioning and position feedback. Details →
[04]Why Soydan

With a large cylinder, confidence rests on documentation.

A mistake on a large bore cylinder is hard to put right, so every stage is documented: material certificates (3.1 to EN 10204 on request), welding procedure specification (WPS), NDT report, buckling calculation and the signed, serialised ISO 10100 test report. The works is certified to ISO 9001, ISO 14001 and ISO 45001 (see downloads). Cylinders we manufacture carry a 12-month warranty from invoice date against defects in material, workmanship and design, under the terms of sale.

The same works builds series cylinders for European OEMs and exports to Germany, Austria and the United Kingdom; our cylinders are also distributed in Europe through Wessel-Hydraulik. Large bore projects run through the same quality system and test procedure. European accounts are handled from our London office, and factory audits in İzmir are welcome by appointment (contact). See also choosing a hydraulic cylinder manufacturer.

[05]Project flow

A large bore cylinder project in six steps.

Each step produces a document; manufacture starts only after you approve the drawing.

01
Application review
Push and pull force, stroke, speed, working pressure, mounting style, installed position and environment.
02
Preliminary design and quotation
Preliminary buckling and strength calculation, proposed construction and main material list; first response within 48 hours.
03
Detail design and approval
2D/3D drawings, weld joint design, seal and guide ring selection; the approved drawing goes under revision control.
04
Material and welding
Honed tube, rod and flange material procured; welding under EN ISO 3834-2, stress relief where required, NDT of welds.
05
Machining, inspection, assembly
Machining, surface and dimensional inspection of the honed tube and chromed rod, and seal fitting; machining, assembly and testing take place at our İzmir works.
06
Test, FAT and dispatch
ISO 10100 pressure test with signed, serialised report; customer-witnessed FAT on request; ISPM-15 crate and lifting plan.

For price factors see hydraulic cylinder cost; for press duty, hydraulic press cylinders.

[06]Illustrative example

Ø630 mm bore, 6 m stroke: how a project is put together.

Illustrative scenario, typical values: a steel plant cylinder with Ø630 mm bore, Ø360 mm rod, 6,000 mm stroke and 250 bar, mounted horizontally in a hot environment. Buckling comes first: a rod that fails the check when pivot-mounted at both ends may pass with a flange mounting and a guided load. The rod, roughly 5 tonnes, sags under its own weight, so guide rings are widened, a stop tube is added and, if necessary, the body is given an intermediate support.

With Ø360 mm confirmed, weld joint design and any post-weld stress relief follow, then sealing: an FKM- and PTFE-based seal set for the heat and a wiper with a metal scraper against scale. Testing to ISO 10100 is at 250 bar and at 1.5 times that, 375 bar. Dispatch needs a lifting plan for the weight and the closed length of over 7 m. This scenario is illustrative, not an actual customer project; for yours, use the quote form.

[07]Frequently asked questions

Large bore cylinders: common questions.

What is the largest bore and stroke you manufacture?

On a project basis: Ø1,000 mm bore, Ø700 mm rod, 12,000 mm stroke and 400 bar working pressure. Standard production runs to Ø400 mm bore and 4,000 mm stroke; anything larger is designed as a project and quoted separately.

Why can large bore cylinders take longer?

Custom cylinders ship ex-works in under 10 weeks from drawing approval. On large bore projects, procurement of honed tube and large-diameter rod material, stress relief and NDT can extend this; the quotation states the project lead time and critical material lead times.

Can you build an equivalent to my existing cylinder?

Yes. Send the dimensions, any drawing (PDF, DWG or STEP) and the operating conditions. We reverse-engineer the design, propose improvements where needed (sealing, bearing arrangement, rod coating) and manufacture after you approve the drawing.

How is testing documented?

The signed, serialised ISO 10100 test report comes with the engineering file. EN 10204 3.1 material certificates and NDT reports are added on request; the pressure test can be witnessed as a factory acceptance test (FAT).

How are shipping, Incoterms and installation handled?

Cylinders ship in ISPM-15 heat-treated crates. We organise freight on request; the Incoterm is agreed per order. Installation and commissioning support by our own teams can be quoted on request.

Describe the project. We will run the numbers.

Send the duty data and any drawings in PDF, DWG or STEP. We reply within 48 hours with an application data sheet.

Request a project quote → WhatsApp